
Tinplate Coating Peeling Risk Analysis and Avoidance Under High-Temperature Retort Sterilization
How High-Temperature Retort Process Damages Can Coating
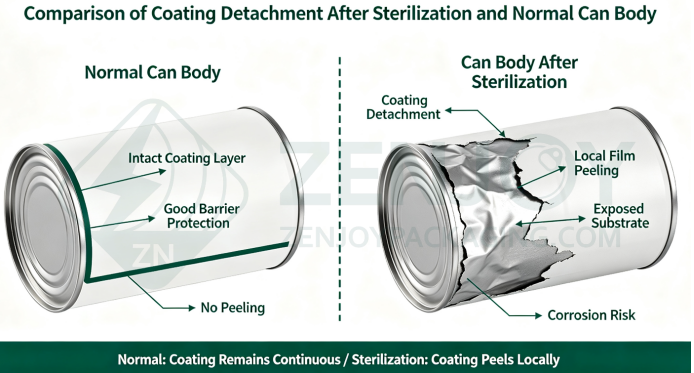
Commercial food can sterilization usually lasts 20 to 60 minutes under 121°C high temperature and saturated steam pressure. During this process, the internal coating faces three major challenges: thermal expansion stress, steam penetration and chemical corrosion from food contents.
If the adhesion between coating and steel substrate is insufficient, thermal expansion will separate the lacquer film from the tinplate surface, forming tiny bubbles. With continuous pressure impact, the bubbles expand and eventually crack, leading to large-area coating peeling after sterilization.
This defect not only destroys the anti-corrosion barrier of the can body, but also causes hidden risks of food contamination and product rejection.
Substrate Root Causes of Tinplate Coating Peeling
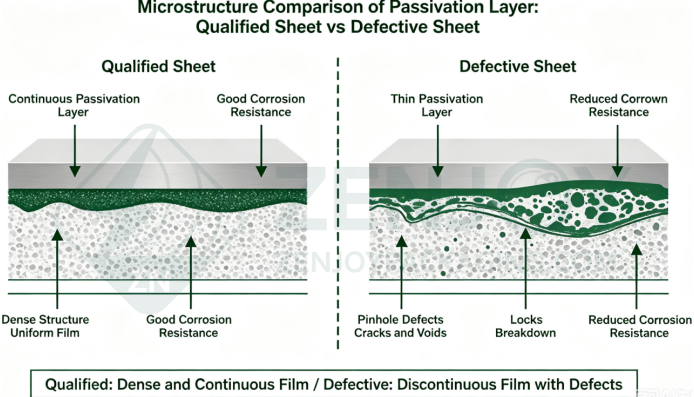
Most high-temperature coating failures originate from material surface defects rather than coating problems.
First, unstable passivation layer. Unqualified tinplate passivation treatment results in loose surface oxide structure. Under high-temperature steam erosion, the bonding force between the substrate and lacquer drops sharply, causing delamination.
Second, uneven tin coating thickness. Local ultra-thin tin layers or coating pinholes lead to inconsistent surface tension. The coating cannot form a uniform and dense protective film, resulting in partial peeling after heating.
Third, residual oil and surface contamination. Insufficient surface cleaning during tinplate production will leave tiny oil stains and dust residues, which greatly reduce lacquer adhesion under high-temperature conditions.
Fourth, improper material grade selection. Ordinary general-grade tinplate cannot withstand repeated high-temperature sterilization cycles. Long-term retort processing will inevitably cause coating fatigue and peeling.
High-Temperature Resistance Difference: ETP vs TFS
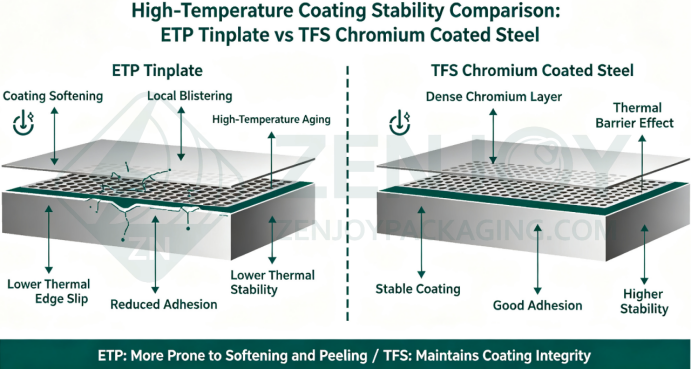
The material difference directly determines the anti-peeling performance under retort conditions.
ETP Tinplate: The pure tin layer is soft and has good ductility, but its high-temperature adhesion is relatively limited. For high-temperature retort cans, ETP requires stricter passivation standards and matched high-temperature resistant lacquer to avoid peeling.
TFS Tin-Free Steel: The chromium oxide composite coating forms a harder and more stable surface structure. It has superior lacquer adhesion and high-temperature resistance. TFS steel is less prone to coating delamination under long-time high-pressure sterilization, making it more suitable for retort-resistant food packaging.
Practical Production Solutions to Avoid Coating Peeling
Combined with actual can-making production experience, standardized material selection and pretreatment can effectively eliminate high-temperature coating peeling defects.
First, select specialized retort-grade tinplate and TFS steel. Ordinary commercial-grade materials cannot meet repeated high-temperature sterilization requirements. Retort-grade materials adopt enhanced passivation technology and strictly controlled surface roughness to ensure stable coating adhesion.
Second, match coating weight according to food attributes. High-humidity and high-protein food cans need higher coating uniformity and optimized surface treatment to resist steam penetration.
Third, control stamping and forming quality. Excessive stretching and friction will damage the base surface and invisible passivation layer, inducing subsequent high-temperature peeling.
As a professional global supplier of tinplate and TFS steel, ZENJOY focuses on solving high-temperature coating stability problems for can manufacturers.
ZENJOY’s retort-grade ETP tinplate and high-adhesion TFS steel adopt standardized enhanced passivation treatment, ultra-clean surface control and uniform coating thickness technology. The materials maintain excellent lacquer bonding performance under 121°C high-temperature sterilization, effectively avoiding blistering, delamination and peeling failures.
Different from ordinary market materials, ZENJOY strictly controls surface roughness, residual oil and passivation uniformity batch by batch, providing stable and reliable substrate guarantee for high-end retort food cans. Whether for fruit cans, meat cans, seafood cans or long-shelf-life preserved food packaging, ZENJOY can provide targeted material grade recommendation and professional technical support to reduce your production defective rate.
Related News
Other news you might be interested in
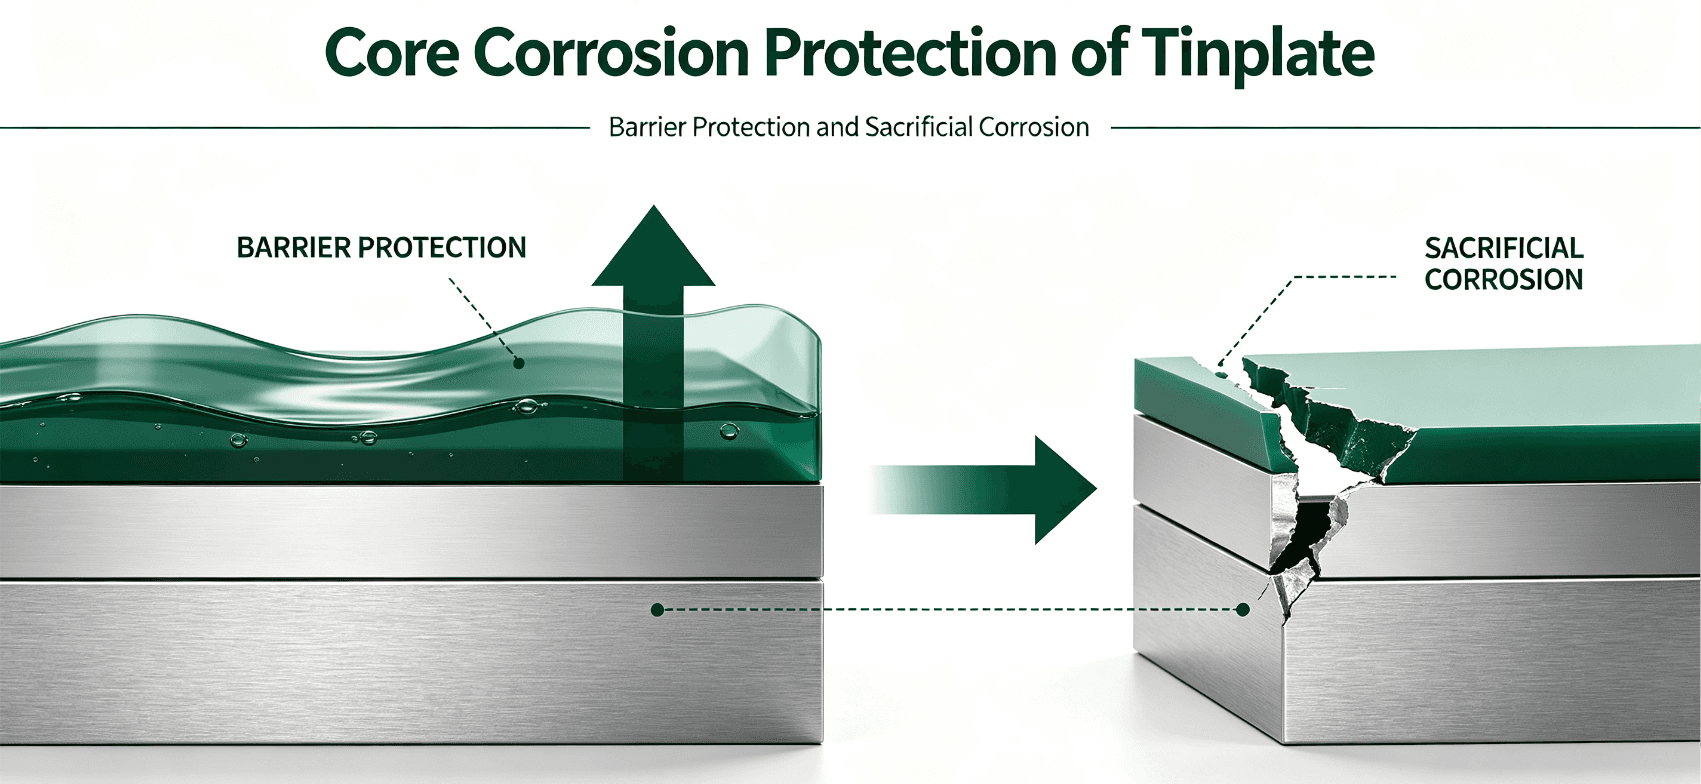
Sacrificial Corrosion & Barrier Protection: Core Anti-Corrosion Principle of Tinplate
The service life and storage safety of metal food cans largely depend on the anti-corrosion performance of packaging materials. As the most widely used substrate for food cans and general metal containers, ETP electrolytic tinplate adopts two core anti-corrosion mechanisms: barrier protection and sacrificial anode protection. These two protection systems work together to ensure stable corrosion resistance in complex food filling and high-temperature sterilization environments.

Sulfuration Black Spot Analysis: Material Causes and Solutions for Food Cans
Sulfuration black spots inside food cans are one of the most common quality puzzles for can manufacturers. Many factories mistakenly attribute the problem to coating or sterilization process issues. In fact, most recurring sulfuration discoloration stems from **incorrect metal substrate selection and surface passivation defects. This article professionally analyzes the essential material causes of can sulfuration black spots, clarifies the performance differences between ETP tinplate and TFS tin-free steel in anti-sulfur scenarios, and provides targeted, actionable solutions for mass can production.
Want to know more?
Get in touch with us for more information about our services and products.